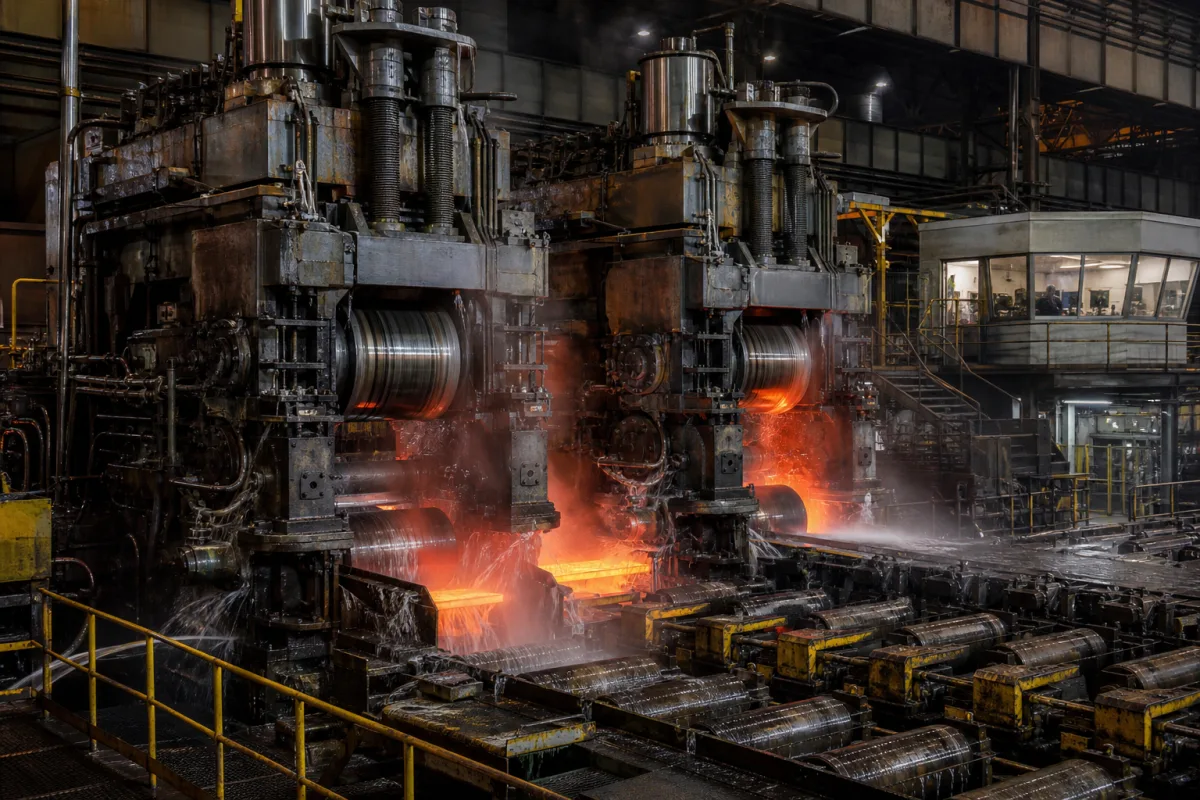
Roughing mill stands in a hot strip mill
Hot strip mills · the reversing stands between reheating furnace and finishing train that turn a slab into a transfer bar
A roughing mill stand is a heavy rolling stand at the head of a hot strip mill. It takes a reheated slab, typically 125 to 280 mm thick in SMS group's data, and rolls it back and forth over several passes into a transfer bar of about 20 to 40 mm that the finishing train then rolls to strip. Modern lines use one or two reversing stands, often a two-high stand followed by a four-high stand, with a vertical edger attached to control width, hydraulic screwdowns to keep the bar straight, and a descaler ahead of them.
Roughing stands, their attached edgers, slab sizing presses and descalers in hot strip mills for steel. Finishing stands, coilboxes and down coilers are covered only where they set limits for the roughing mill; plate mills and section mills are different machines.
01
From slab to transfer bar: the roughing stand's share of the reduction
In SMS group's hot strip mill brochure, the hydraulic adjusting systems are rated for slabs of 125 to 280 mm and for finished strip of 1 to 25.4 mm, and the coilbox that receives the roughed product is rated for transfer bars of 20 to 40 mm at 900 to 1,100 °C. Most of the thickness is therefore taken out in the roughing stands. [1]
| Line | Roughing arrangement | Source |
|---|---|---|
| HBIS Laoting, China (SMS group, full production 2021) | Two roughing stands, edger attached to the second, slab sizing press at the roughing mill entry [2] | SMS press release |
| Usiminas Hot Strip Mill No. 2, Brazil (Primetals, hot run March 2012) | One 4-high reversing roughing mill (R2) with hydraulic gap control and an entry-side vertical edger [3] | Primetals article |
| SMS group reference stand | Four-high reversing rougher with edger [1] | SMS brochure |
The Laoting mill shows what the roughing stands feed: a seven-stand finishing train designed for roll forces of 52 MN (F1–F4) and 40 MN (F5–F7), producing 4.1 million t a year of coil up to 1,900 mm wide and 1.2 to 25.4 mm thick. [2]
Editorial calculation from the SMS ranges: rolling a 250 mm slab to a 35 mm transfer bar removes 215 mm, or 86% of the thickness, before the finishing mill takes the bar from 35 mm to a few millimetres. [1]
02
Hydraulic screwdowns and edgers: what keeps the transfer bar straight and on width
SMS describes the roughing stand's hydraulic horizontal adjusting cylinders, working with hydraulic side guides and their automation, as the means of minimising camber and wedge so that transfer bars come out straight. Width is held from head to tail by hydraulic edger adjustment with a fast dynamic response, which trims cropping losses; the latest edgers are fully hydraulic with no extra electromechanical adjustment. [1]
| Adjusting system (SMS data) | Speed | Force |
|---|---|---|
| Horizontal, roughing and finishing stands | Up to 12 mm/s | Approx. 50,000 kN [1] |
| Vertical (edger), per side | Up to 60 mm/s | Up to 8,000 kN [1] |
SMS lists redundant position and force measurement on the horizontal adjustments, digital position measurement and proven cylinder seals, and states that more than 40 mills have received its hydraulic adjusting systems since 2000. [1]
Primetals' Usiminas R2 pairs the same two functions, hydraulic gap control on the four-high stand and a vertical edger on its entry side. [3] A roughing stand quoted at only a few thousand kN would sit an order of magnitude below these screwdown ratings; ask the builder for the design rolling force, the edger force and the screwdown stroke of the stand on offer.
03
Taking width out before the roughing passes: sizing press or edger
A slab sizing press at the roughing mill entry squeezes the slab edges with tools that move with it. SMS claims width reductions of up to 350 mm in one pass and, against a conventional edger, better forming through to the slab centre with flatter dogbones, so less width springs back in the following flat passes. Laoting uses one to roll from slabs held in stock to the widths customers order. [1] [2]
| Sizing press figure | SMS value |
|---|---|
| Sizing force | 22,000 kN [1] |
| Width reduction | Up to 350 mm [1] |
| Drive power | 4,400 kW [1] |
| Feed rate | Up to 300 mm/s [1] |
| Slab thickness | Up to 280 mm [1] |
| Slab width | 650 to 2,300 mm [1] |
| Slab length | 4 to 12 m [1] |
| Slab temperature | 1,250 °C [1] |
SMS reports 21 sizing presses installed in hot strip mills and says they can be added to existing mills in short shutdowns. Where no press is fitted, the attached edger alone sets width, within the force and speed in the table above. [1]
04
Descaling ahead of the roughing stand
Scale left on the slab is rolled into the surface, so a descaler sits upstream of the roughing mill as well as before the finishing train. SMS rates its descalers for material 650 to 2,200 mm wide and 15 to 280 mm thick at 0.15 to 2.0 m/s, with water at up to 400 bar and 200 to 700 m³/h. [1]
The spray headers and water troughs are height-adjustable to suit material thickness, and nozzles are arranged to even out cooling between top and bottom faces; ask for the header count, pressure at the nozzle and the water station's capacity when the roughing passes need intermediate descaling. [1]
05
Enquiry for a roughing stand or rougher rebuild
These points follow from the figures above. [1] [2]
- Slab range: thickness, width, length, weight, temperature at the furnace exit
- Transfer bar target: thickness and width range, temperature at the coilbox or finishing entry
- Stand layout: number of roughing stands, 2-high or 4-high, reversing or not, passes per stand
- Design rolling force, screwdown type (hydraulic or electromechanical plus hydraulic), stroke and speed
- Edger: force and speed per side, attached or free-standing; whether a sizing press is wanted
- Descaler: positions, pressure, flow
- Main drive power and speed for the heaviest pass schedule
- Rebuild limits: foundations, housing reuse, shutdown length
06
Request for a roughing mill stand
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Mill: [line name; annual tonnage; product mix]
Slabs: [thickness; width; length; temperature]
Transfer bar: [thickness; width]
Stands: [number; 2-high/4-high; reversing]
Forces: [rolling force; edger force; screwdown speed]
Width control: [edger; sizing press; width reduction]
Descaling: [pressure; flow; headers]
Scope: [new stand / rebuild; drives; automation]
Roughing mill builders
Roughing stands are built by the metallurgical plant makers as part of a hot strip mill or a rebuild; the lines cited here were supplied by SMS group and Primetals Technologies.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Buyer questions
What does a roughing mill stand do in a hot strip mill?
It rolls a reheated slab, 125–280 mm thick in SMS group's data, over several reversing passes into a transfer bar of about 20–40 mm for the finishing mill. [1]
How many roughing stands does a hot strip mill have?
Often one or two: HBIS Laoting has two with an edger on the second, Usiminas No. 2 has a single four-high reversing stand R2 with an entry edger. [2] [3]
What force does a roughing stand screwdown apply?
SMS lists horizontal hydraulic adjusting systems for roughing and finishing stands at approximately 50,000 kN and up to 12 mm/s; edgers reach up to 8,000 kN per stand at 60 mm/s per side. [1]
What is the difference between a sizing press and an edger?
A sizing press reduces slab width by up to 350 mm in one pass with forming through to the centre; an edger rolls the edges with vertical rolls and is quicker to react but takes less width. [1]
Sources and what still needs a direct check
Sources checked 2026-11-09T05:04:52+08:00. Equipment ranges come from the SMS group hot strip mill brochure W4-305E (2019); plant layouts from SMS group's 2021 press release on HBIS Laoting and a Primetals article on Usiminas Hot Strip Mill No. 2. All values are maker data.
- SMS group — Hot strip mills: equipment brochure W4-305E (slab sizing press, hydraulic adjusting systems, coilbox, descalers), 2019 ↗ Manufacturer brochure Return to text ↑
- SMS group — Press release: HBIS Laoting starts full production of the new high-performance hot strip mill (8 April 2021) ↗ Manufacturer press release (copy) Return to text ↑
- Primetals Technologies — Superior mill performance: advanced hot strip mill (Usiminas Hot Strip Mill No. 2) ↗ Manufacturer article Return to text ↑
Still to check yourself
- Get the design rolling force of the stand offered.
- Match transfer bar thickness to the finishing mill and coilbox.
- Decide between edger alone and sizing press.
- Check descaler pressure and flow for the pass schedule.
Request manufacturing insight for Roughing Mill Stands
Ask for use case, specification boundaries, supplier type, and RFQ preparation information for this product.
- Where it goes
- Straight to the CNFX editorial desk, and to the manufacturer if this product is linked to a claimed profile. Nothing is broadcast to a supplier list.
- Your details stay here
- We do not sell or rent enquiry data, and we do not add you to a mailing list. Used only to answer this request.
- No commission, no middleman
- CNFX is a directory. We take no cut of any order and never negotiate on a supplier's behalf.
- What to include
- Share your product specifications, quantity, destination and target delivery date.
Need to Manufacture Roughing Mill Stands?
Compare manufacturer profiles with relevant product and process capability.