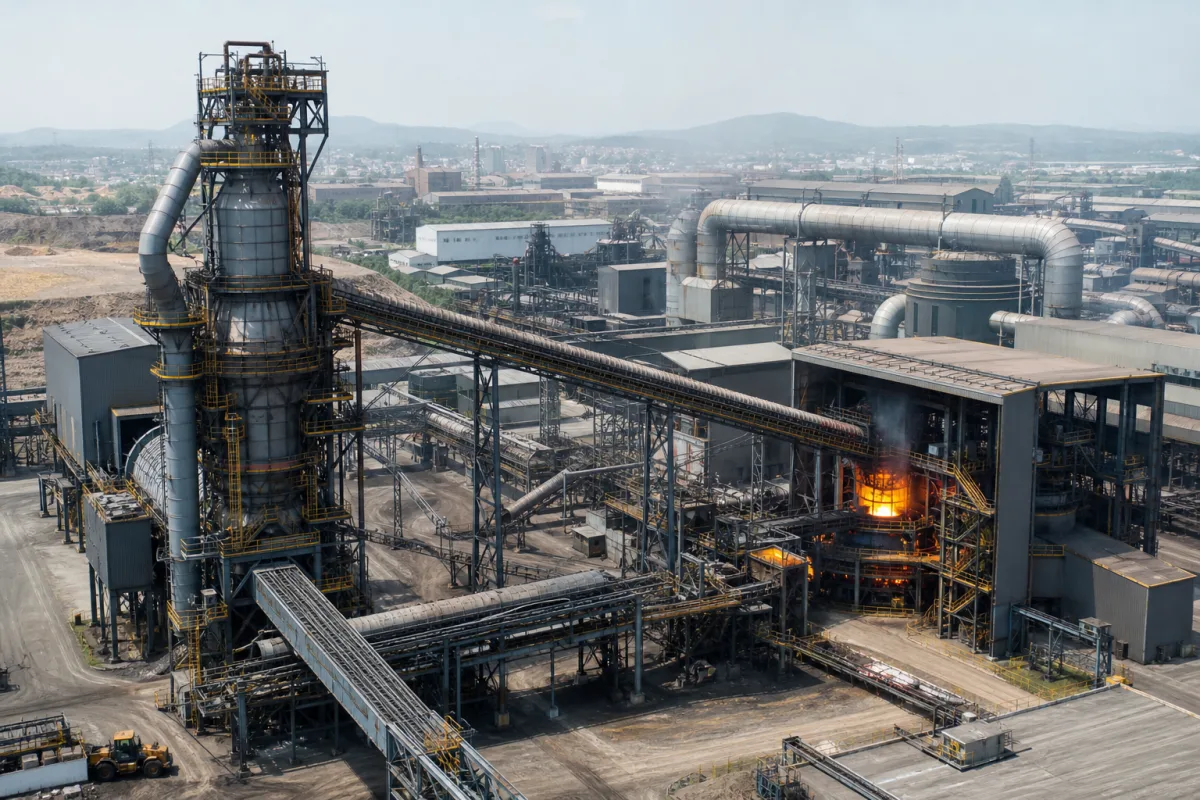
DRI–EAF steelmaking route: charging direct reduced iron to the electric arc furnace, cold or hot
Where the shaft furnace meets the melt shop · what changes in the arc furnace when DRI replaces scrap, how DRI metallization and gangue set the feed rate, and hot DRI carried to the furnace at 600 °C
A DRI–EAF plant turns iron ore pellets into steel in two linked units: the shaft furnace removes the oxygen from the ore without melting it, and the electric arc furnace melts the resulting direct reduced iron (DRI) into steel. The shaft furnace is specified on its own page; this page is about the link and the melt shop behind it. DRI is not scrap: it carries gangue oxides and carbon, it is fed continuously through the furnace roof rather than in baskets, and its temperature on arrival can be ambient or, on a hot link, around 600 °C. Each of these changes the arc furnace's energy, time per heat, slag volume and yield.
Integrated direct reduction and electric arc furnace steelmaking: the DRI or HBI transfer from the reduction plant to the melt shop (cold, hot conveyor or pneumatic), continuous DRI feeding to the arc furnace, and the EAF operating figures that DRI changes. Gas-based shaft furnace plants are covered on the Direct reduction shaft furnace page and their discharge equipment on the Discharge system for a direct reduction shaft furnace page; arc furnaces as stand-alone equipment are on the Electric arc furnace page and their electrode control and process models on the Process control system for electric arc furnace steelmaking page. The blast furnace route as a whole is on the Integrated blast furnace–basic oxygen furnace steelmaking system page. Pelletizing and secondary metallurgy are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 3 sources
Arc furnace figures with 60–95% DRI against 100% scrap
Kirschen, Hay and Echterhof (University of Bayreuth and RWTH Aachen) give typical production ranges for low-alloyed steel grades; their slag data cover 16 industrial EAFs of 60 t to over 200 t tap weight. [1]
All values from table 2 of the paper. [1] The authors explain the differences: DRI carries 4–7 wt% gangue oxides and 1.5–4.3 wt% carbon; it is fed continuously through the fifth hole in the roof at 50% to over 95% of the charge, onto a hot heel that, depending on shell design, reaches up to 30% of the melt; without a scrap pile the arcs run shorter at lower voltage with slightly lower energy transfer; and extra lime and doloma to hold slag basicity at 1.8–2.1 can raise slag to 140 kg/t, each kilogram of burned slag former adding about 0.37–0.50 kWh. [1] HBI, by contrast, is charged with scrap in buckets and needs only minor changes up to about 10% of the charge. [1]
Editorial calculation: moving from 30 to 60 kg/t of slag formers at 0.37–0.50 kWh/kg adds about 11–15 kWh/t, a small part of the 140–340 kWh/t gap between the two energy ranges in the table.
Parameter
100% scrap charge
80–95% DRI charge
Share of DRI/HBI (%)
0–5 (HBI)
60–95 (DRI)
Electric energy (kWh/t)
340–390
530–680
Natural gas (m³/t)
5–10
0–2
Oxygen (m³/t)
25–37
20–35
Coal and carbon fines (kg/t)
2–9
8–17
Slag formers — lime, doloma (kg/t)
23–35
27–60
Tap temperature (°C)
1600–1635
1600–1635
Tap-to-tap time (min)
50–60
60–100
Metal yield (%)
90–94
87–92
02
Feed rate from DRI quality: metallization, gangue and carbon
Alameddine and Bowman modelled the energy needed to melt DRI from its analysis and used it to set the continuous feed rate that keeps bath temperature constant at a given arc power. They give the world range of DRI analyses as 89.2–94% total Fe, 88–96% metallization, 0.3–4% C, 1–5% SiO₂, 0.5–3% Al₂O₃, 0.1–2% CaO and 0.1–1% MgO. [2]
The authors find metallization to be the main variable for the feed rate, with gangue having a weak influence on feed rate but a strong one on yield. [2] Kirschen and co-authors list DRI from six production sites ranging from 1.7 to 4.3 wt% carbon and from 81.5% to 96.0% metallization. [1]
Editorial calculation: 28.6 kg/MW·min at 100 MW is 2,860 kg of DRI a minute, about 172 t an hour; a 2-point error in assumed metallization at that rate is what produced the 50 °C drift in the model, which is why the DRI analysis has to reach the melt shop's control system, not only the quality lab.
About 2.6 kWh in DRI practice, where the oxygen generates “almost exclusively CO”, against 5.2 kWh in scrap melting, at 100% thermal efficiency [2]
Balanced feed rate example
28.6 kg/MW·min for DRI with 5% gangue, 2.1% C and 90% metallization [2]
Effect of ±2% metallization at that feed rate
Bath temperature drift can exceed 50 °C after 10 minutes (100 MW, 50 t liquid steel, 7.5 t slag) [2]
Effect of gangue
Liquid steel yield can drop by about 7% as gangue rises from 3% to 8% [2]
Specify the DRI analysis the arc furnace is designed for — metallization, carbon, gangue and its CaO/SiO₂ ratio — and how often each lot's analysis is sent to the furnace control.
03
Hot DRI to the furnace: pneumatic transport at 600 °C
Energiron describes HYTEMP as a pneumatic system that carries hot DRI from the reduction plant directly to the EAF or an open slag bath furnace while keeping it at about 600 °C, to reduce the arc furnace's electrical energy use. It states the system has been in operation since 1998 and reports no DRI fines losses from the system. [3]
Alameddine and Bowman report steel shops charging DRI hot and that the reduction in energy comes from the enthalpy the hot DRI carries, normalised in their data to the percentage of DRI charged and its temperature. [2] Kirschen and co-authors list DRI as charged cold or hot through the roof. [1]
For a buyer, the hot link fixes the plant layout — the distance and height between the shaft furnace discharge and the EAF roof — and adds a second operating mode to plan for: what the melt shop does with DRI when the arc furnace is down, and how cold DRI or HBI is fed when the hot link is out of service.
04
Data for a DRI–EAF link enquiry
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
DRI: [metallization; carbon; gangue and CaO/SiO₂; size; cold, hot or HBI]
Share: [DRI % of charge; scrap and HBI mix]
Arc furnace: [tap weight; transformer MW; hot heel; fifth-hole feeding rate]
Targets: [kWh/t; tap-to-tap; yield; slag kg/t]
Transfer: [conveyor or pneumatic; temperature at the furnace; distance and height]
Control: [DRI analysis to furnace control; feed-rate model]
Operation: [mode when the EAF or the hot link is down]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
How much more electricity does an EAF use on DRI?
Kirschen et al. give 530–680 kWh/t for 60–95% DRI heats against 340–390 kWh/t on scrap; Alameddine and Bowman found averages of 683 and 583 kWh/t. [1][2]
How is DRI fed to the arc furnace?
Continuously through the fifth hole in the furnace roof, at 50% to over 95% of the charge, onto a hot heel that can reach 30% of the melt depending on shell design. [1]
Why does DRI metallization matter?
In Alameddine and Bowman's model, a ±2% change in metallization at a 28.6 kg/MW·min feed rate drifted bath temperature by over 50 °C in 10 minutes. [2]
Can DRI be charged hot?
Yes; Energiron's HYTEMP pneumatic system carries hot DRI to the EAF at about 600 °C and has operated since 1998. [3]
Sources and what still needs a direct check
Sources checked 2026-10-12. EAF operating ranges from Kirschen, Hay and Echterhof, Processes 9 (2021) 402; DRI melting model from Alameddine and Bowman, Archives of Metallurgy and Materials 53 (2008); hot DRI transport from Energiron's HYTEMP page.