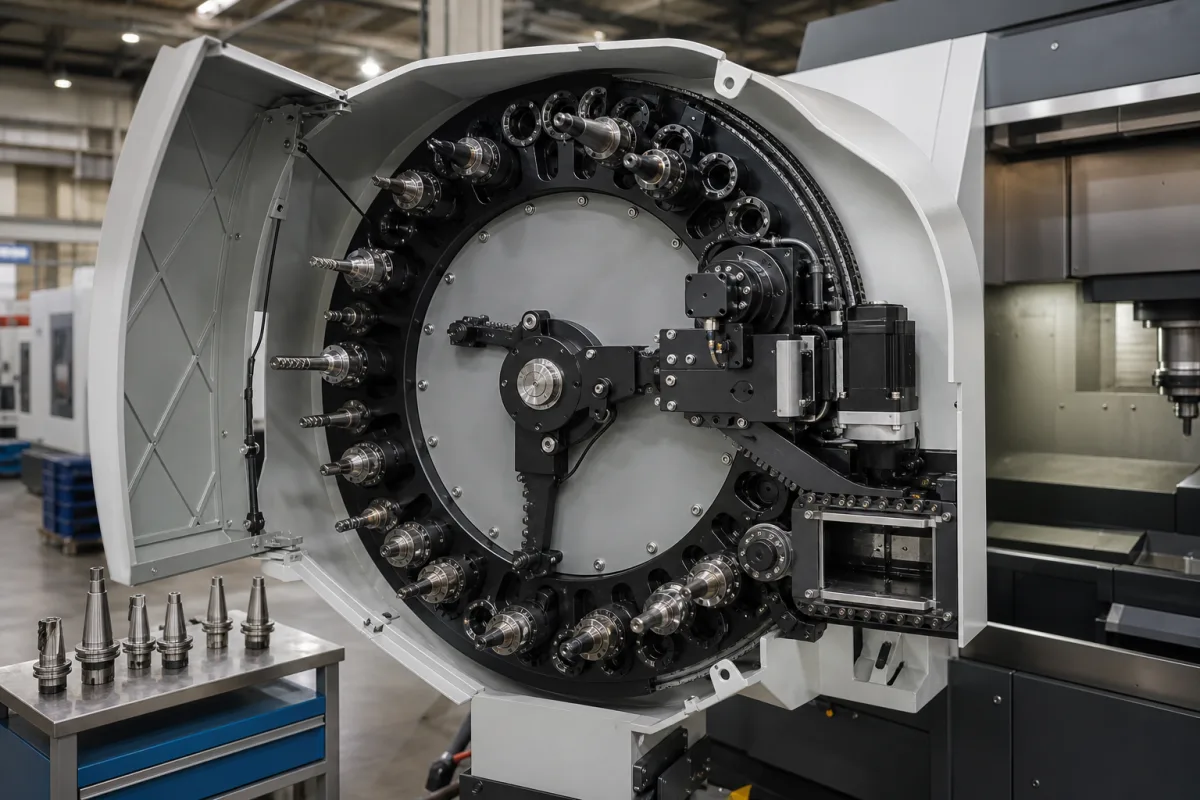
CNC tool magazines · Taper and capacity, maximum tool diameter full and with empty neighbours, tool weight and length, change time
A CNC tool magazine is the drum, disc or chain store on a machining centre that holds tool holders in numbered pockets and indexes the requested tool to the change position, where an arm or the spindle exchanges it. Ask three things first: which taper and how many pockets you need, how large, long and heavy your biggest tools are and whether they need empty pockets beside them, and how long a tool change takes.
Drum, disc and chain tool magazines with their tool change mechanisms for CNC machining centres, supplied fitted or as components. Lathe turrets, robot tool changers, tool holders alone and tool presetters are outside this page.
CNFX editorial research · Sources checked October 12, 2026 · 5 sources
TAC Rockford's datasheet for drum and disc automatic tool changers lists, by taper: BT/CAT/ISO 30 or HSK32A with 20 tools, 5.0 kg maximum tool weight, 250 mm length and 60 mm diameter; 40-taper or HSK63A with 20 or 24 tools, 6.5 kg, 300 mm, and 97 mm diameter for 20 tools or 81 mm for 24 with all pots full; a 30-tool 40-taper version at 85 mm; and 50-taper or HSK100A with 20 or 24 tools, 15.0 kg, 350 mm, and 133 or 125 mm diameter. [1]
The datasheet shows the trade-off between capacity and tool size: more pockets on the same 40-taper drum means a smaller full-pocket diameter. [1] One Chinese vertical machining centre listing gives a 24-tool magazine with φ80 × 300 mm tools when full, φ150 × 300 mm when adjacent pockets are empty, and 8 kg maximum tool weight. [2]
Editorial note: list your largest face mills, boring heads and long drills with diameter, length and weight, including holder, and check each against the magazine's full-pocket and empty-neighbour limits and its maximum weight before ordering.
Give the supplier the spindle taper, number of tools, the largest tool diameters, lengths and weights including holders, which tools need empty neighbouring pockets, required tool change time, tool identification, and whether the magazine is fitted to a new machine or retrofitted.
02
Plan usable capacity and change time
TAC Rockford gives tool change times of 1.2 s for its 30-taper unit, 1.8 s for the 40-taper units and 2.5 s for the 50-taper unit, all at 60 Hz, with electric power for both magazine and changer. [1]
Editorial calculation: on a 24-pocket magazine like the one above, four large tools that each need both neighbouring pockets empty use up to 12 pockets if placed apart, leaving 12 for normal tools, so usable capacity falls from 24 to about 16; placing big tools two pockets apart lets them share empty pockets. [2]
A published design study shows how change time depends on where the next tool sits. Gökler and Koç (Middle East Technical University; International Journal of Machine Tools & Manufacture 37(3):277–286, 1997) designed a disc-type tool changer for a horizontal machining centre built by a CNC machine tool manufacturer. After comparing alternatives, they chose a disc magazine with 24 tools, a maximum tool diameter of 150 mm and a maximum tool weight of 8 kgf; the changer exchanges the closest tool within 4 s and the farthest within 6 s. [3]
Editorial note: when a supplier quotes a single tool change time, ask whether it is for the adjacent pocket or the farthest one; in the study above the difference was 2 s per change. [3]
Editorial calculation: a part needing 40 tool changes at 1.8 s spends 72 s in tool changes alone; compare suppliers' tool change and chip-to-chip times for your cycle. [1]
03
Check the total tool mass limit as well as the per-tool limit
FANUC America lists tool specifications for two of its ROBODRILL BBT30 vertical machining centres. The "α D14S i B5 ADV Plus" holds 14 tools of up to 200 mm length, 80 mm diameter and 4 kg each, with a total mass of 30 kg and a 0.7 s tool change time; the "α D28L i B5 ADV Plus Y500" holds 28 tools of up to 250 mm length, 80 mm diameter and 4 kg each, with a total mass of 46 kg and the same 0.7 s. Both list an air pressure of 72 psi / 0.5 MPa. [4][5]
The total mass line limits how many heavy tools can be loaded at once. On FANUC's figures the per-tool limit times the number of pockets exceeds the total mass on both machines, so a magazine full of tools at the 4 kg maximum is not allowed [4][5]. TAC Rockford's data sheet gives per-tool limits by taper [1]; ask any supplier whether a total magazine load limit also applies, and plan heavy tools against it.
Tool change time is quoted differently by each source. FANUC gives one figure, 0.7 s, for both machines [4], TAC Rockford gives 1.2 s for its 30-taper unit [1], and the METU disc magazine design reports 4 s for the nearest and 6 s for the farthest tool [3]. Ask whether a quoted time is tool-to-tool or chip-to-chip and for which pocket distance.
Editorial calculation: 14 tools at 4 kg would weigh 56 kg against the 30 kg total, so the average tool in a full magazine can weigh at most about 2.1 kg (30 ÷ 14); for the 28-tool machine, 112 kg at the per-tool limit against 46 kg total gives about 1.6 kg average (46 ÷ 28). [4][5]
Item
FANUC α D14S i B5 ADV Plus
FANUC α D28L i B5 ADV Plus Y500
TAC Rockford 30-taper ATC (already cited)
Number of tools
14
28
20
Max tool length
200 mm
250 mm
250 mm
Max tool diameter
80 mm
80 mm
60 mm
Max tool mass
4 kg
4 kg
5.0 kg
Total mass
30 kg
46 kg
—
Tool change time
0.7 s
0.7 s
1.2 s
Holder
BBT30
BBT30
BT/CAT/ISO 30 or HSK32A
Values are from FANUC America's ROBODRILL model pages; FANUC does not state on those pages whether the change time is tool-to-tool or chip-to-chip.
04
Compare what suppliers offer
Suppliers linked to this page list tool magazines or machining centres with them; each card links to the page reviewed.
Listings include tool magazines among machine tool accessories, and vertical machining centres fitted with 24-tool magazines.
05
Trace the magazine components
This is a functional reference built from the sources cited; it is not one maker's specification.
Fill the specification fields with values for your tools
A tool magazine quotation needs values for your tools. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 13 October 2026
Buyer questions
How big a tool fits in a tool magazine?
It depends on capacity and neighbours: TAC lists 97 mm for 20 tools and 81 mm for 24 on 40 taper; one 24-tool VMC allows φ150 mm with neighbours empty. [1][2]
How heavy can tools be?
TAC lists 5.0 kg for 30 taper, 6.5 kg for 40 taper and 15.0 kg for 50 taper. [1]
How long does a tool change take?
TAC lists 1.2 s (30 taper), 1.8 s (40 taper) and 2.5 s (50 taper) at 60 Hz. [1]
Does tool change time depend on which pocket the next tool is in?
Yes. In a 24-tool disc design for a horizontal machining centre, the closest tool changed within 4 s and the farthest within 6 s. [3]
Can every pocket of a tool magazine hold a tool at the maximum weight?
Not always. FANUC lists its ROBODRILL α D14S i B5 ADV Plus at 4 kg per tool but 30 kg total for 14 tools, and the 28-tool α D28L i B5 ADV Plus Y500 at 46 kg total, so a full magazine of maximum-weight tools exceeds the limit. [4][5]
Sources and what still needs a direct check
Sources checked 2026-10-12. TAC Rockford sells machine tool components and publishes figures for its own drum and disc changers; the Asiatools listing (also a supplier below) describes one machine's magazine.