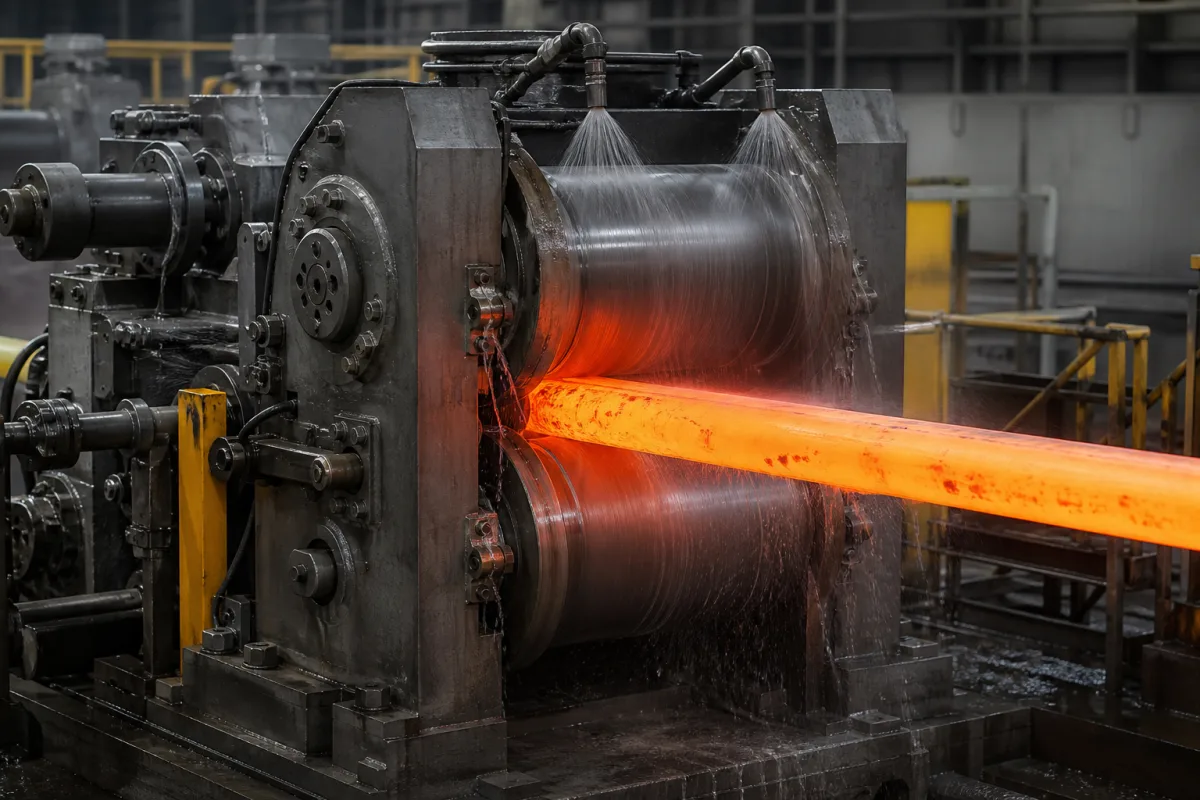
Caster pinch roll pair and its clad roll face: thermal-fatigue cracking under spray water, Type 420, austenitic and laser-clad overlays, and re-cladding
Continuous casting · the driven roll pair that grips the hot strand under cooling sprays, and the weld-clad surface that decides how long the rolls last between regrinds
A pinch roll on a caster grips a strand whose surface is still hot enough to glow, while water from the sprays runs over the roll face. Each revolution heats the contact line and quenches it again, and the roll face cracks, corrodes and wears until the stand has to come out. This page looks at the roll pair from its working surface: the weld cladding, a few millimetres to a few centimetres deep, its alloy, how it was welded and heat treated, and how much of it is left for regrinding.
The rolls of continuous-caster pinch roll (withdrawal) stands for billets, blooms and slabs, considered from the roll face: thermal-fatigue and corrosion cracking under spray water, weld-clad and laser-clad surface alloys, heat treatment of the cladding, and regrinding and re-cladding of worn rolls. Withdrawal force, dummy-bar handling and straightening strain are covered on the Withdrawal and straightening unit of a billet caster page; using withdrawal rolls for soft reduction on the Withdrawal unit as a soft-reduction stand page; strand guide segments, roll pitch and single-piece or shell guide rolls on the Strand guide system for continuous casters page; complete casters on the Billet continuous caster page; spray nozzles and headers on the Secondary cooling (spray) zone of a continuous caster page, and foot-roller supports on the Secondary-cooling spray chamber structure and foot-roller support for continuous casters page; spray-cooled work rolls of hot strip mills on the Work rolls under spray cooling in hot strip finishing stands page.
CNFX editorial research · Sources checked October 13, 2026 · 3 sources
Spray water, steam and radial cracks: how a caster roll face spalls in about four months
Two roll-surfacing patents describe the service the roll face sees and the way it fails.
AG Industries' patent on caster roll claddings lists the conditions: cyclic thermal shock, thermal and mechanical bending stresses and elevated-temperature abrasion; a strand surface that may exceed 1,204 °C at the first caster roll and is quenched between rolls; cooling water carrying acids or bases from the flux and water-treatment chemicals; and a roll that elongates at the contact line, so it goes through tension–compression cycles. [1] It names pinch rolls among the rolls its method applies to, alongside table, tension and hot and cold work rolls. [1]
Armco's overlay patent describes the crack pattern. Thermal fatigue produces radial surface cracks on the roll, from which side cracks form; cooling water trapped in the cracks and turned to steam on each revolution helps them grow; and side cracks off the main radial cracks, principally in the second weld layer, link up and cause spalling of the roll surface after about four months. [2] AG Industries traces the start of the cracking to corrosion pits in the reheat regions next to the weld interbead areas, where chromium carbides form at prior austenite grain boundaries as each bead overlaps the last and leave planes of chromium depletion that lose passivity. [1]
Ask how the offered rolls are clad and heat treated, what crack depth the supplier regrinds out, and how many months of service the same cladding has given on comparable stands.
02
Type 420 by submerged arc, nitrogen-alloyed austenitic overlay or laser-clad Rockit 485
Three overlay routes appear in the sources; each was published by the party offering it, so the comparison claims below are the publishers' own.
Höganäs developed Rockit 485 for caster rolls in the bending segment, which it singles out, together with the foot roll at the mould exit, for the extreme conditions there. [3] Pinch rolls in the withdrawal stand are not named in its sheet, so its figures describe the overlay, not a tested pinch roll. Armco's own wear test put its austenitic overlay ahead of tempered Type 420 in metal-to-metal wear. [2]
Overlay
Composition as published
Welding and heat treatment
Hardness and stated performance
AISI Type 420 martensitic stainless, submerged arc
Over 0.15 % C, 12.00–14.00 % Cr, Mn and Si 1.00 % max. [2]
A cited reconditioning practice preheats the roll to at least 600 °F at 150 °F per hour and holds it there through welding; martensitic overlays need stress relieving [2]
HRC 50 (typ.) for the grade, per Armco [2]; an as-deposited test overlay reached HRC 59, harder to machine and more prone to crack [2]
Nitrogen-alloyed austenitic stainless (Armco)
About 0.015–0.10 % C, 6.0–10.0 % Mn, 13.0–20.0 % Cr, 1.0 to under 3.5 % Ni, 0.12–0.22 % N [2]
No preheat or post-weld stress relief on low-carbon rolls; two to four layers, the first partly martensitic from dilution, the third free of martensite [2]
Softer as welded, work-hardens in service; costed at about 35 % less than a Type 420 overlay for the same service life, but Armco states it has not overcome crack propagation from thermal fatigue in caster-type service [2]
Fe bal., 0.15 C, 13.0 Cr, 4.5 Co, 4.0 Ni, 2.8 Mo, 0.8 Nb, 0.6 Si wt% (typ.) [3]
Höganäs lists no need for preheating or post-weld heat treatment; tests with dilution from the substrate below 5 % [3]
43–49 HRC; Höganäs claims higher resistance to oxidation, corrosion and thermal fatigue than SAW martensitic overlays, and shows corrosion resistance 10 times that of SAW and PWHT AISI 420 in its acidic polarization test [3]
Ask for the overlay alloy and process, layer count and finished thickness, the hardness after heat treatment, and whether the hardness and corrosion data quoted were measured on the offered process or on test coupons.
03
Regrinding and re-cladding: a 0.05 cm diameter tolerance and up to 1.3 cm of diameter to machine away
AG Industries' patent gives the dimensions that frame roll refurbishment.
Caster rolls in that document range from 15 to 48 cm in outside diameter with body lengths of 25 to 230 cm, and are hollow with a centre bore for water cooling of the bearings. [1] The protective cladding is about 0.1 to 2.5 cm thick, and the roll diameter must not vary by more than about 0.05 cm because of the tolerances on strand thickness; a small change of the surface from wear, thermal shock or corrosion shuts the casting operation down so the roll assembly can be removed and its rolls remachined or re-surfaced. [1] Weld beads are about 1.3 to 7.6 cm wide and 0.13 to 0.32 cm thick, with three complete layers given as an example. [1]
The patent's method heats the cladding by a scanning induction coil, at about 300 Hz to 5 kHz, to between about 870 °C and 1,260 °C to dissolve the carbides, then cools it so that the interbead zones are no longer sensitized, leaves the cladding in compression, and aims at cladding deep enough for a used roll to be machined down by up to 1.3 cm of diameter without re-heat treating. [1] Editorial calculation: 1.3 cm off the diameter removes 0.65 cm from the radius, so only claddings toward the thicker end of the 0.1 to 2.5 cm range leave clad material at the surface after the full regrind allowance. [1] Armco describes rebuilding cracked rolls by machining the cracks into tapered cavities, filling them, and overlaying again. [2]
Give the roll diameter, body length and bore, and ask for the finished cladding thickness, the regrind allowance on diameter before re-cladding, and the heat treatment applied after each re-cladding.
04
Data for a caster pinch roll enquiry
Paste it into your enquiry below or into an email to a maker, then replace every bracket.
Caster: [billet, bloom or slab; strand size; casting speed]
Roll: [diameter; body length; bore and cooling; journal and bearing arrangement]
Surface: [overlay alloy wanted or offered; process (SAW, laser); finished thickness]
Heat treatment: [preheat; post-weld treatment; target hardness]
Service: [spray water chemistry; current life between regrinds; crack and spalling pattern]
Refurbishment: [regrind allowance; re-cladding cycles; inspection after regrind]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Share this page
Compiled and source-reviewed by the CNFX editorial team.
Each manufacturer above links to the page on that company's own website where the product is listed, with the date we checked it. How we source and review
· Page last updated 13 October 2026
Buyer questions
Why do caster pinch and guide roll faces crack?
Armco's patent describes thermal fatigue producing radial cracks, cooling water turning to steam in them on each revolution, and side cracks linking up to spall the surface after about four months; AG Industries traces crack starts to corrosion pits in chromium-depleted reheat zones between weld beads. [2][1]
What overlay is used on caster rolls?
Armco's patent describes conventional rolls with a ferritic or martensitic stainless overlay, naming AISI Type 420; it also describes a nitrogen-alloyed austenitic overlay, and Höganäs offers a laser-clad Fe-based powder, Rockit 485, at 43–49 HRC. [2][3]
How much can a clad roll be reground?
AG Industries' patent aims at cladding deep enough to machine a used roll down by up to 1.3 cm of diameter, within a diameter tolerance of about 0.05 cm in service. [1]
Does a laser-clad overlay need preheating?
Höganäs lists no need for preheating or post-weld heat treatment with Rockit 485, against a 600 °F minimum preheat in a cited Type 420 reconditioning practice. [3][2]
Sources and what still needs a direct check
Sources checked 2026-10-13. Two US patents, from AG Industries on induction treatment of caster roll claddings and from Armco on an austenitic overlay, describe roll service, failure and surfacing; Höganäs' Rockit 485 sheet gives composition, hardness and process data for a laser-clad overlay.