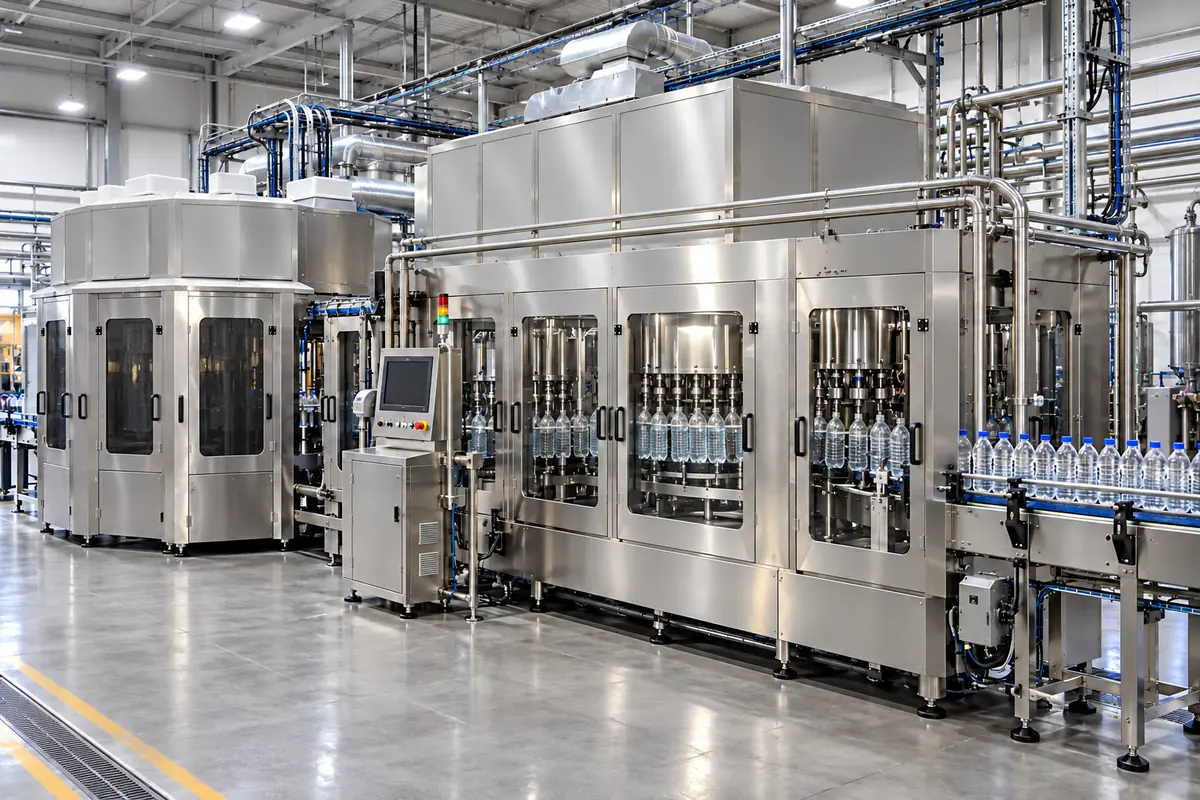
Blow-fill-cap combiblocks for PET bottles · stretch blow moulding, filling and capping in one enclosure, no empty-bottle conveying or accumulation, aseptic and hot-fill versions, output from 12,000 to 54,000 bottles per hour, and the line around the block
A blowing-filling-capping combiblock is a single machine block that stretch-blow-moulds PET bottles from preforms and passes them directly, without conveyors, to a filler and capper inside the same enclosure. Ask three things first: which products and fill type (still, carbonated, hot or aseptic) it must handle, what bottle sizes and output it needs, and which upstream and downstream machines complete the line.
Integrated blow-fill-cap (combi) blocks for PET bottles for water, carbonated soft drinks, juices, dairy, edible oil and similar, including aseptic and hot-fill versions. Stand-alone blow moulding machines (a separate product page), stand-alone fillers and cappers, glass and can lines, and blow-fill-seal machines for pharmaceutical ampoules are outside this page except where compared.
CNFX editorial research · Sources checked October 12, 2026 · 5 sources
Sidel, which says it introduced the Combi concept in 1997, describes it as combining blow moulding, filling and capping in an integrated system within a PET packaging line: by eliminating conveying, empty-bottle handling, accumulation and storage, Combis optimise line layout with a smaller footprint, improving production hygiene and efficiency while lowering operating costs, with capping applied within the same enclosure. Its range includes combis for water and still or pulpy beverages with preservatives, a hot-fill combi integrating heat-resistant blowing, hot filling and capping in one enclosure, and aseptic combis using dry preform and cap decontamination or wet bottle decontamination. [1]
Editorial note: with no accumulation between blower and filler, a stop at the filler or capper affects bottle production directly; ask the supplier how the block handles a downstream stop, how many preforms or bottles are rejected, and how changeovers between bottle sizes are done.
Give the supplier the products and fill type (still water, carbonated, juice with or without pulp, hot fill, aseptic), bottle sizes and shapes with preform drawings, neck finish and closure type, required output in bottles per hour per size, fill accuracy and level, hygiene class, available compressed air, cooling and power, downstream equipment (labeller, packer, palletiser), changeover frequency, and site layout.
02
Size the output and the line around the block
King Machine, a filling line maker linked to this page, describes its blowing-filling-capping combiblock, designed for bottled water, with output from 12,000 to 54,000 bph to customer need, naming 18,000, 24,000 and 36,000 bph as example sizes, servo blow moulding, preform and cap electrostatic dust removal, bottle neck camera inspection and stable preform and bottle transfer. Its typical water line places the combi blower/filler/capper with a cap feeder and washer, inspection, dryer, labeller, date coder, shrink packer, palletiser and stretch wrapper; its juice line adds a cap sterilizer and bottle cooler, and its CSD line a mixer and bottle warmer. [2]
KHS's data sheet for the InnoPET BloFill stretch blow molder/filler/capper monoblock (with Blomax Series IV, edition September 2015) gives a fuller technical envelope: bottle content 0.2–3.0 l, bottle height 120–360 mm and diameter 40–125 mm; capacity up to 81,000 bph for still beverages and up to 72,000 bph for carbonated ones; a blow molder of 8 to 36 cavities; fillers of 40 to 144 filling stations for still and 48 to 192 for carbonated beverages; filling temperature 4–20 °C; and fill-level accuracy of s = 1.0–3.0 ml. It lists NIR preform heating, servo-controlled stretch bars, an airlock in the transfer to the filler, separated wet and dry areas and quick-change format parts, with hot filling, UV treatment, dry-air blow moulding and camera inspection as options. [3]
Editorial calculation: 72,000 bph from a 36-cavity blow molder is 2,000 bottles per cavity per hour, or one bottle per cavity every 1.8 s (3,600 ÷ 2,000); at 81,000 bph a 144-station still filler completes about 563 fills per station per hour. Ask which cavity and valve count a quoted output assumes. [3]
Editorial calculation: 24,000 bottles per hour is 24,000 / 60 = 400 bottles per minute; with 500 ml bottles the block fills 24,000 × 0.5 = 12,000 L, or 12 m³, of product per hour, which sets water treatment, mixing and cooling capacity upstream. Output and bottle size are assumed examples; ask for the rated output for every bottle size.
03
Weigh the maker's efficiency and space claims for a tribloc
SIPA, an Italian PET equipment maker, describes its "Sincro Bloc" as integrating bottle blowing, filling and capping in a single system for still and carbonated, cold-fill and hot-fill products, with and without pulp, including C.S.D. without preservatives and products that need weight filling. Its newer "Sincro Tribloc" adds a roll-fed labeller between blower and filler: it connects the XTRA rotary blower, the XLABL roll-fed labeller and the FLEXTRONIC electronic filler, eliminating intermediate conveyors, for production of up to 90,000 bottles per hour. [4][5]
These are SIPA's own figures, and the release does not state the test basis for the efficiency, space or cost numbers [5]. Sidel makes a similar case for its Combi, that eliminating conveying and accumulation gives a smaller footprint and better hygiene [1], and KHS publishes output by product type for its InnoPET BloFill [3]. Ask each supplier for the bottle, product and fill temperature behind a quoted output, how line efficiency was measured, and the layout drawing used for any space comparison.
Adding the labeller inside the block changes the changeover and maintenance picture as well as the footprint: SIPA says accessibility around the labelling area was improved [5]. If the line runs more than one label format, ask for the label changeover time on the tribloc against a separate labeller, and how a labeller stop affects the blower and filler.
Editorial calculation: at 3,000 bottles per hour per cavity, 90,000 bottles per hour needs at least 30 blowing cavities (90,000 ÷ 3,000); at 95% line efficiency a nominal 90,000 bph gives about 85,500 bottles per running hour. [5]
Item (SIPA Sincro Tribloc)
Published value (maker claim)
Output
Up to 90,000 bottles per hour
Blower speed per cavity
3,000 bottles per hour per cavity (XTRA rotary blower)
Blowing process angle
275°
Lightweight example
4.9g for a 0.5-liter format
Overall line efficiency
95%
Space
Up to 30% less than traditional standalone equipment
Operating cost
Up to 15% savings in overall operating costs
Material
Fully compatible with 100% rPET
Values are from SIPA's Sincro Bloc product page and its Sincro Tribloc news release; they are maker claims and no data sheet was reviewed.
04
Compare what suppliers offer
Suppliers linked to this page list blow-fill-cap combiblocks; each card links to the page reviewed.
Listings include water, CSD, hot-fill, aseptic, ultra-clean and big-container combiblocks and blowing-labeling-filling-capping blocks, and combiblocks for bottled water within complete filling lines. Ask each for output by bottle size, fill type, changeover time and references for similar products.
05
Trace the combiblock modules
This is a functional reference built from the sources cited; it is not one maker's specification.
Fill the specification fields with values for your line
A combiblock quotation needs values for your line. The table explains each field, gives published values where a reviewed source states them, and says what to obtain from the supplier.
Field
What it means and published values
Ask the supplier for
Output
Example: 12,000–54,000 bph; up to 81,000 (still) / 72,000 (CSD) bph; up to 90,000 bph tribloc. [2][3][5]
Output per bottle size.
Bottle range
e.g. 0.2–3.0 l, 120–360 mm high, 40–125 mm diameter. [3]
Explore company information and manufacturing capabilities, then discuss the scope of your project with a relevant supplier.
Compiled and source-reviewed by the CNFX editorial team.
Published product pages show what a company offers, not tested performance. Confirm the legal seller, factory and scope for your order. How we source and review
· Page last updated 12 October 2026
What does a blow-fill-cap combiblock remove from a line?
Sidel says it eliminates conveying, empty-bottle handling, accumulation and storage, giving a smaller footprint and better hygiene. [1]
How fast are combiblocks?
King Machine quotes 12,000 to 54,000 bph for water combiblocks, naming 18,000, 24,000 and 36,000 bph as example sizes. [2]
Are there aseptic and hot-fill combis?
Yes; Sidel lists hot-fill combis and aseptic combis with dry or wet decontamination. [1]
How many blow cavities and filling valves does a high-output combiblock use?
KHS's InnoPET BloFill data sheet lists 8 to 36 blow cavities and 40 to 144 (still) or 48 to 192 (carbonated) filling stations, for up to 81,000 or 72,000 bottles per hour. [3]
What is a blow-label-fill tribloc?
SIPA's Sincro Tribloc connects a rotary blower, a roll-fed labeller and an electronic filler in one block without intermediate conveyors, for up to 90,000 bottles per hour, with SIPA claiming 95% line efficiency and up to 30% less space than standalone machines. [5]
Sources and what still needs a direct check
Sources checked 2026-10-12. Sidel and King Machine are packaging machine makers describing their own combiblocks; their figures and benefits are maker statements.